:sales@zsjhsteelgroup.com WhatsApp:+86-15122582058





| Quantity: | |
|---|---|


ZSJH
Large-Diameter, Thick-Wall Pipe for Pipeline and Structural Projects
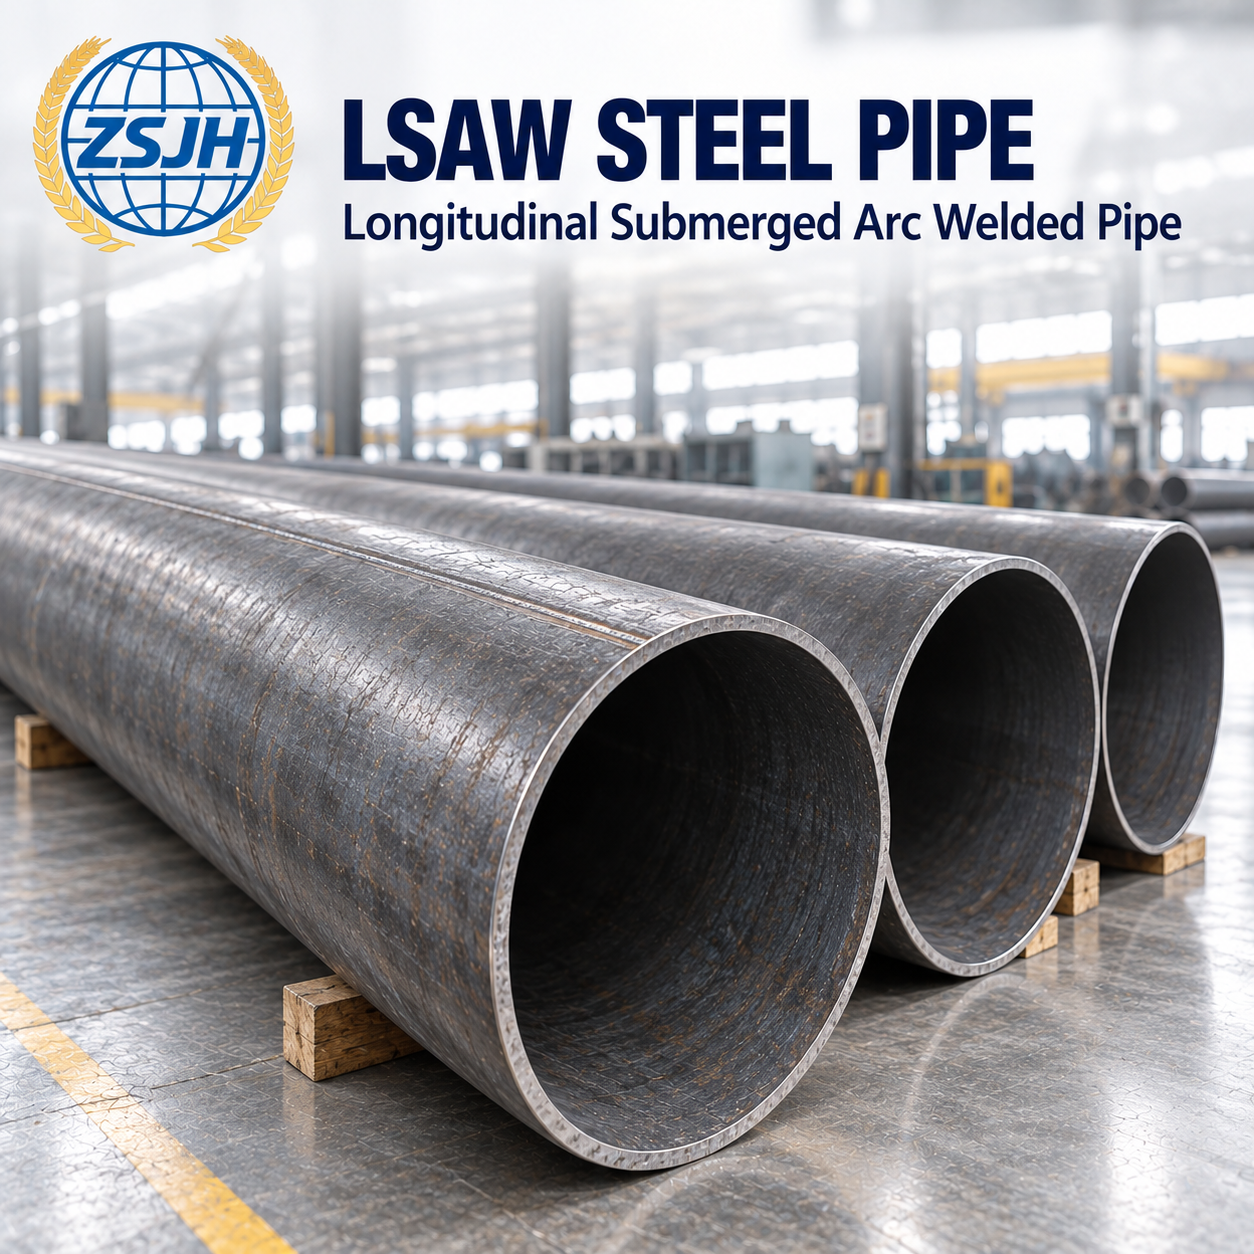
LSAW Steel Pipe, also known as SAWL pipe, is manufactured by forming steel plate into a cylindrical section and joining the longitudinal edges through submerged arc welding. Common forming routes include JCOE and UOE, with mechanical expansion used to improve dimensional consistency.
This manufacturing process supports large-diameter and thick-wall pipe production for oil and gas transmission, water infrastructure, large structural members and engineering pipelines. Suitability depends on the selected standard, steel grade, design conditions and inspection requirements.
A typical manufacturing sequence includes plate inspection, edge preparation, forming, tack welding, internal and external submerged arc welding, dimensional correction, inspection and pipe-end finishing. The exact sequence varies by manufacturing route and product specification.
JCOE Forming
Steel plate is progressively pressed into J, C and O shapes, welded longitudinally and mechanically expanded.
UOE Forming
Steel plate is formed into a U shape and then an O shape, followed by longitudinal welding and mechanical expansion.
Key product features include:
Large-diameter production: Suitable for projects requiring substantial flow capacity or large tubular sections.
Thick-wall options: Plate-based manufacturing accommodates demanding wall thickness requirements within the qualified production range.
Longitudinal submerged arc weld: Internal and external welding produces a continuous straight seam.
Dimensional control: Forming, sizing and expansion help control diameter, ovality and pipe-end geometry.
Project-specific finishing: Pipe ends, coatings, inspection and documentation can be specified for the intended service.
Diameter and wall thickness must be assessed together with steel grade, forming capability, pipe length and testing requirements. The maximum available diameter and maximum wall thickness should not be assumed to be available in every combination.
For a suitable supply proposal, specify:
| Parameter | Details to Confirm |
|---|---|
| Outside diameter | Required diameter and permissible variation |
| Wall thickness | Nominal thickness, tolerance and any minimum-wall requirement |
| Length | Fixed or random length and cutting tolerance |
| Geometry | Ovality, straightness and pipe-end dimensional requirements |
| Steel grade | Required strength level and material specification |
| Pipe ends | Plain or beveled ends, including bevel angle and root face |
| Surface protection | Bare steel, temporary protection or specified coating system |
For welded pipeline installation, pipe-end dimensions and bevel consistency are particularly important for fit-up and field welding.
Steel grade selection should reflect the project’s strength, toughness, weldability and operating requirements.
For line-pipe procurement, API 5L designations such as Grade B, X42, X52, X60, X65 and X70 may be specified, subject to manufacturing qualification and availability. Where applicable, the order must also identify the product specification level, delivery condition and supplementary requirements.
Higher-strength grades do not automatically provide better suitability for every project. Material selection should consider:
Design pressure and temperature
Required wall thickness and corrosion allowance
Impact toughness and minimum design temperature
Field welding procedures
Sour-service requirements, where applicable
Applicable pipeline or structural design rules
LSAW describes the manufacturing process; it does not by itself establish pressure rating, toughness or suitability for sour service.
Weld integrity is a central requirement for LSAW pipe. Plate-edge preparation, welding consumables, welding parameters and alignment must be controlled through qualified manufacturing procedures.
Depending on the applicable standard and inspection plan, examination may include:
Ultrasonic testing: Examination of the weld and relevant adjacent areas for specified discontinuities.
Radiographic testing: Examination of required weld sections or locations in accordance with the specified acceptance criteria.
Pipe-end examination: Additional inspection of end areas where required.
Plate examination: Inspection for laminations or other relevant material discontinuities when specified.
Visual inspection: Assessment of weld profile, surface condition and workmanship.
Testing methods, coverage, inspection stages and acceptance criteria must be agreed before production. A statement such as “NDT tested” should be supported by a defined inspection scope and traceable records.
Hydrostatic testing verifies the pipe’s ability to withstand a specified internal test pressure under controlled conditions. For orders requiring this test, the pressure, holding time and acceptance criteria follow the governing specification and approved project requirements.
Test planning should account for pipe dimensions, material grade and the applicable calculation rules. Required records should identify the tested pipe or production lot as specified.
Hydrostatic test pressure is not the same as the allowable operating pressure. Operating limits must be established through the project design.
Oil & Gas Transmission
For onshore or offshore pipeline projects when the manufacturing qualification, steel grade, toughness, testing and corrosion protection meet the project specification. Offshore and sour-service applications require additional technical review.
Water Transmission
For bulk water pipelines, pumping systems and major water infrastructure. Internal lining and external coating should be selected according to water quality, installation conditions and service requirements.
Large Structural Members
For tubular columns, piles, supports and other engineered structural components. Structural suitability depends on the selected specification, connection design, loading and corrosion protection.
Engineering & Industrial Pipelines
For project pipelines requiring large bores, substantial wall thickness or defined material and inspection requirements.
Pipe ends can be specified as plain or beveled to suit fabrication and installation requirements. Bevel geometry, end squareness and any local weld dressing should be confirmed before production.
Depending on project requirements and confirmed availability, protection options may include external epoxy, 3LPE or 3LPP systems, together with suitable internal coatings or linings. Surface preparation, coating thickness, inspection and uncoated end lengths should be defined in the order.
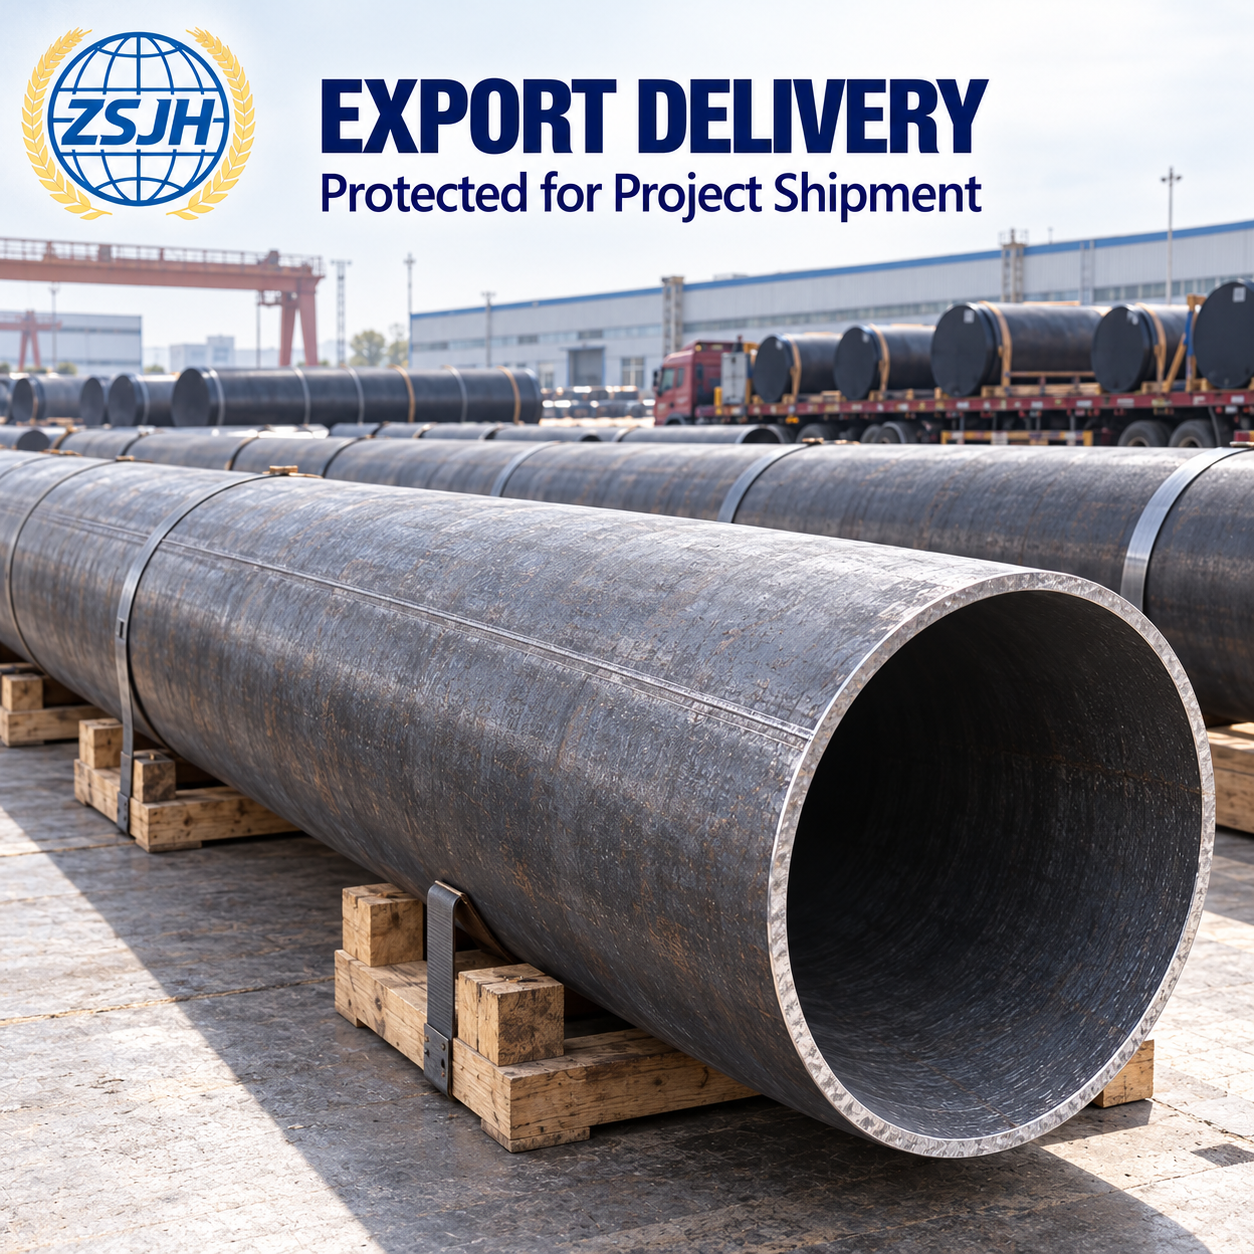
Large-diameter pipes require suitable handling and shipment arrangements. Timber supports, chocks, restraints and end protection should be selected to limit movement and protect pipe geometry and finished surfaces during transport.
ZSJHSTEEL helps overseas buyers coordinate LSAW pipe sourcing around project specifications, rather than dimensions alone.
We work with your required steel grade, diameter, wall thickness, weld inspection scope, hydrostatic testing, coating and shipping requirements to develop a suitable supply proposal. Confirming these details early supports clearer quotations, consistent documentation and more efficient receiving inspection.
What is the difference between LSAW and SSAW pipe?
LSAW pipe has a longitudinal weld and is typically formed from steel plate. SSAW pipe has a spiral weld and is typically formed from steel strip. Selection depends on the project specification, dimensions, grade and qualified manufacturing route.
Are JCOE and UOE pipes interchangeable?
Both are forming routes for longitudinally welded pipe. Acceptance depends on the project specification and manufacturer qualification; some projects restrict the permitted manufacturing route.
Can large diameter and heavy wall thickness be supplied together?
Availability depends on the complete combination of diameter, thickness, grade and length. Submit the full specification for a feasibility review.
Does every order include ultrasonic testing and hydrostatic testing?
The required tests and their scope follow the applicable standard and purchase order. Confirm testing requirements and documentation before placing the order.
Can LSAW pipe be used for drinking water?
It may be suitable when the pipe system and all water-contact materials, including the lining, meet the relevant drinking-water requirements. Bare steel pipe alone does not establish compliance.
Please provide:
Application and destination country
Product standard, edition, steel grade and specification level
Outside diameter, wall thickness, length and quantity
Required dimensional tolerances
Design temperature and any toughness or sour-service requirements
Weld NDT methods, coverage and acceptance criteria
Hydrostatic testing and documentation requirements
Pipe-end preparation, coating and lining specifications
Inspection certificate or third-party inspection requirements
Destination port and delivery schedule
Contact ZSJHSTEEL to discuss LSAW Steel Pipe dimensions, material grades, inspection requirements and export supply options.


